A topology optimized part can be totally wrong.
That is the idea in a recent research review of topology optimization (TO), generative design (GD), and additive manufacturing. The software can remove material from low stress regions and create an elegant lattice structure. But the resulting shape may need way too many supports, possibly trap powder, distort during a metal build, or be basically impossible to inspect properly.
In other words, the fancy topology optimizert software may have done exactly what it was asked to do. The problem is that it might not have been asked enough.
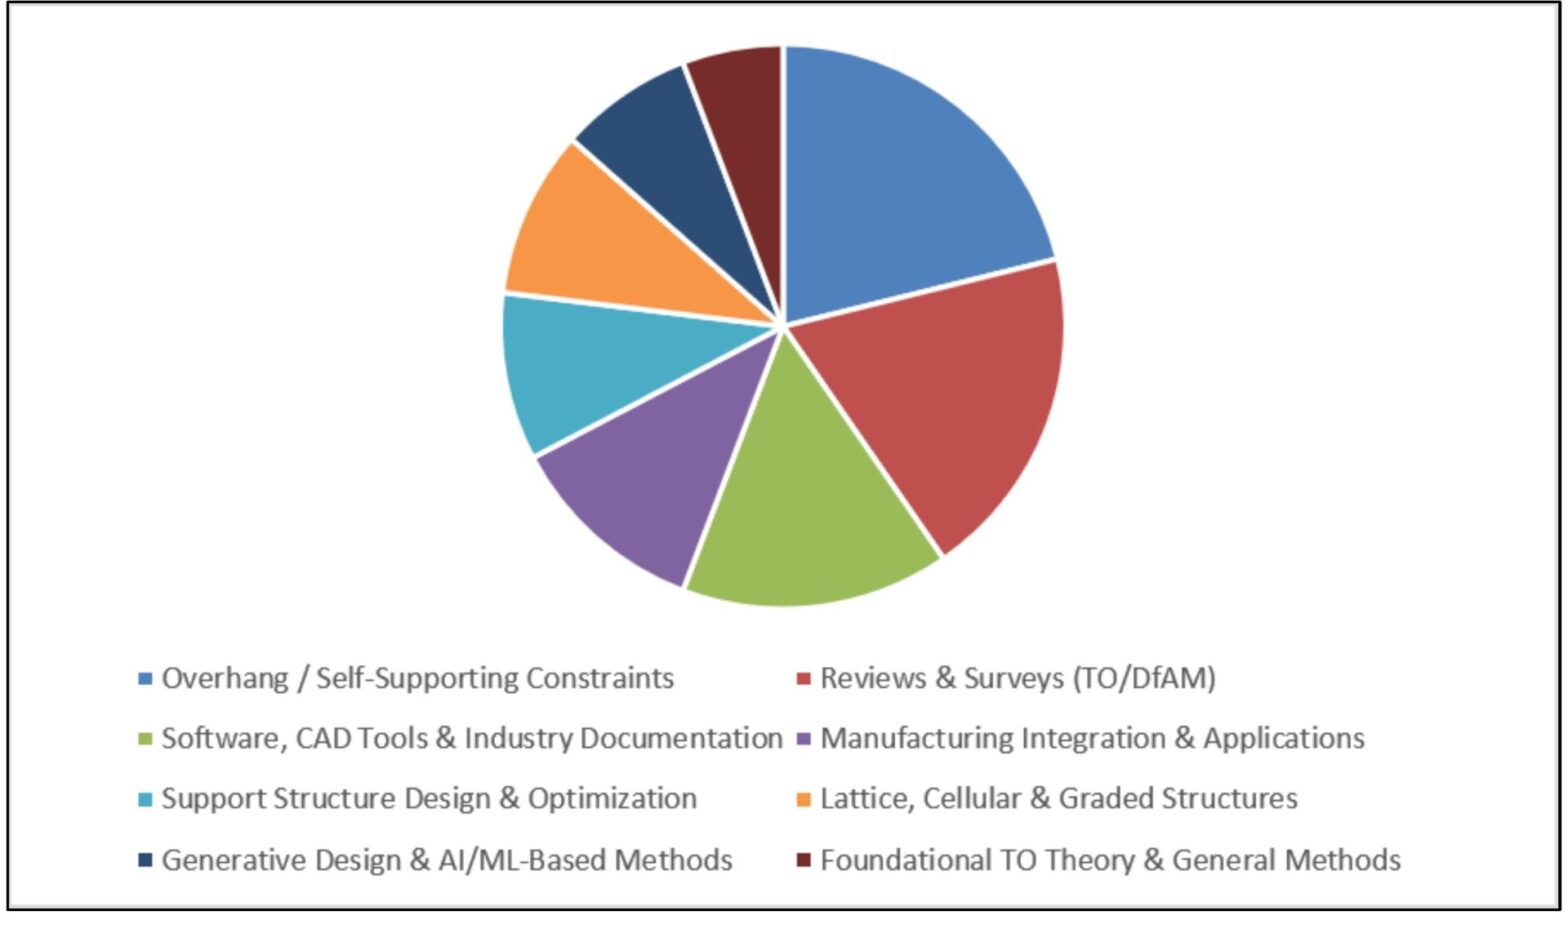
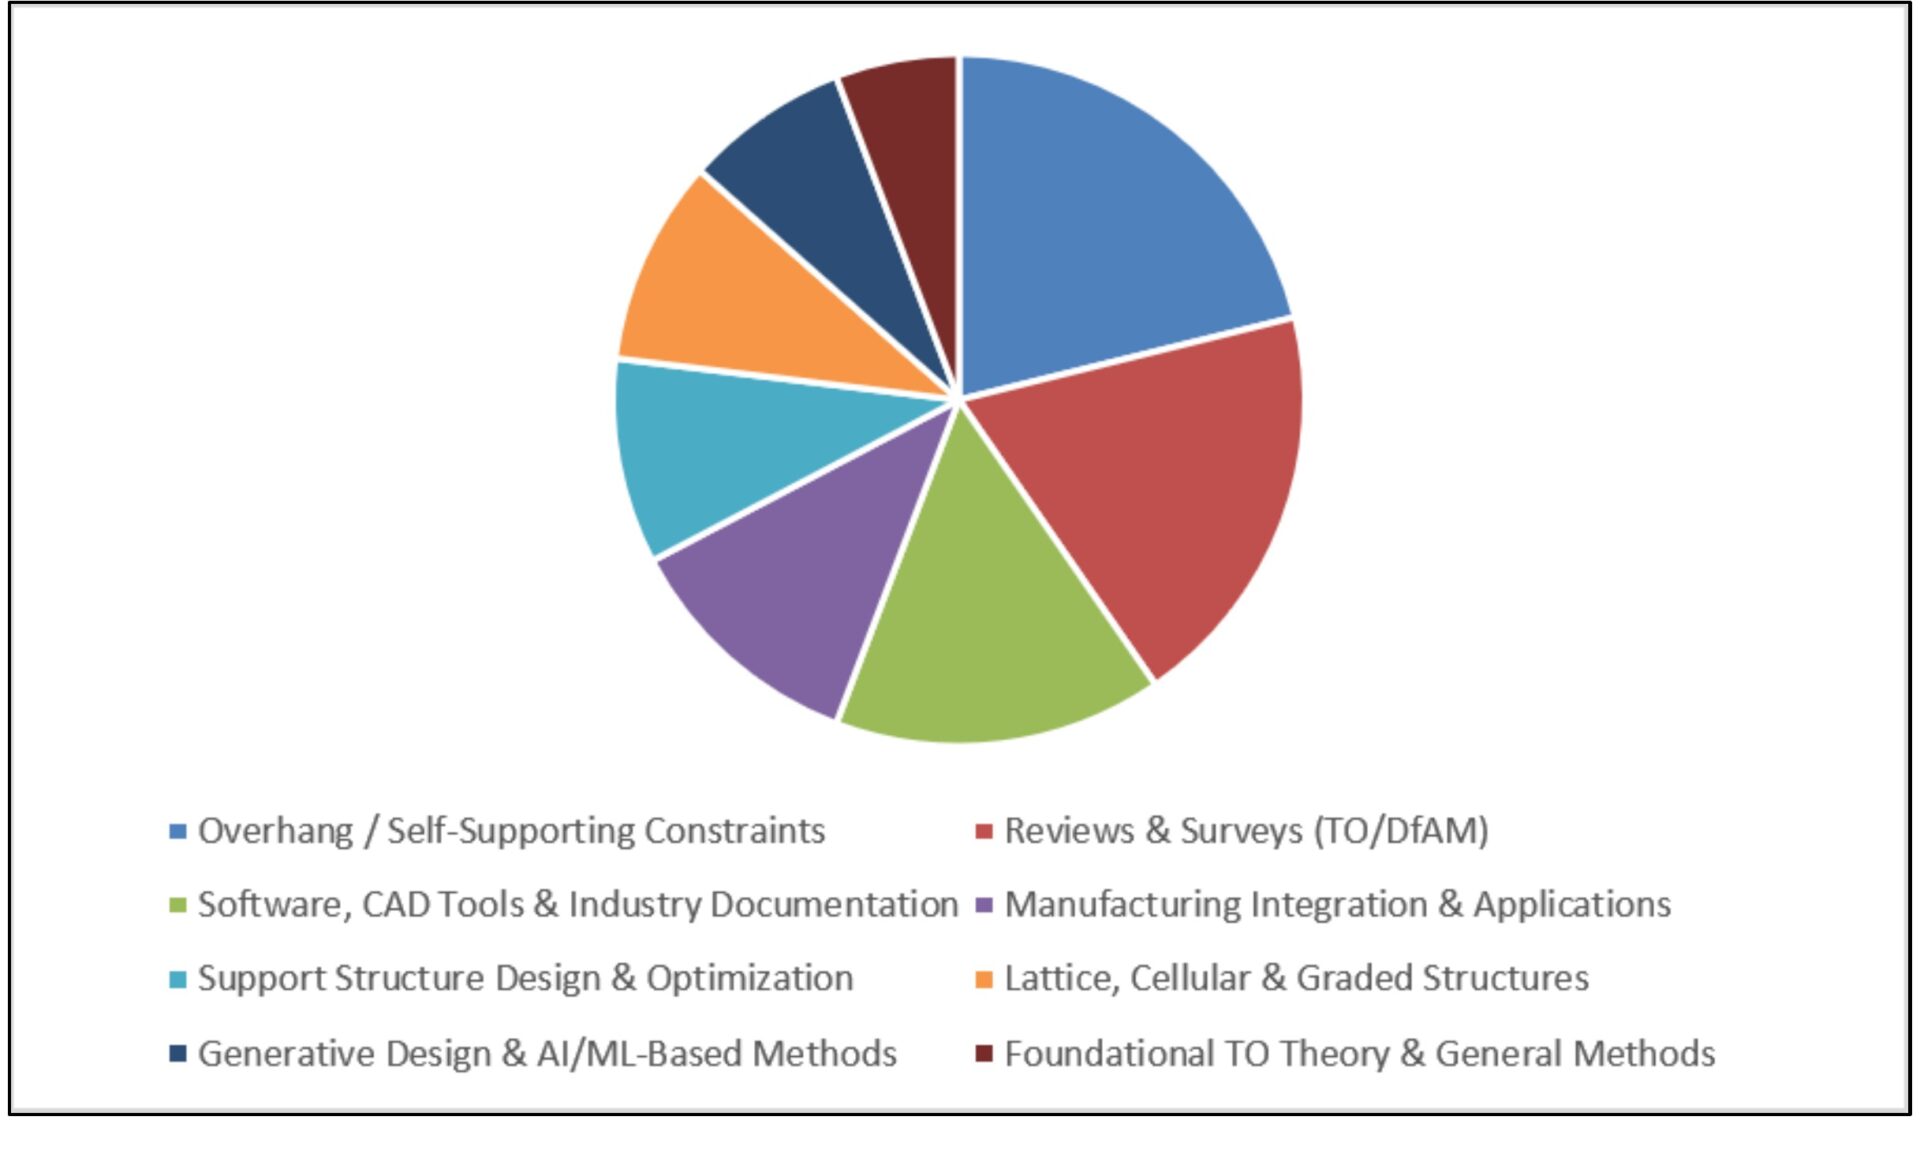
The research review by Arnold Dumisani Sibanda and colleagues examined 54 looked at sources across nine themes, including self-supporting structures, support optimization, lattices, thermal effects, software, and AI-assisted methods.
TO and GD are often thought of as the same thing, but the paper says otherwise. TO is the mathematical part: distribute a limited amount of material inside a defined design space to meet objectives such as stiffness, weight, frequency, or thermal behavior. Generative design is the larger workflow around it, potentially including material choice, interfaces that must remain untouched, simulation, lattice generation, manufacturing rules, and comparison of many candidate designs.
Neither one is a replacement for engineering judgement, of course. At least, not yet anyway.
A typical TO run commonly assumes an ideal material: uniform, isotropic, and with predictable elastic properties. Actual AM parts are often none of those things. Metal parts can carry residual stresses and direction-dependent properties developed during their creation. Material extrusion parts behave differently depending on extrusion direction, layer bonding, infill, and layer height.
It’s even more problematic when optimization produces thin walls and unusual joints. Those are exactly the features most likely to expose a difference between the material assumptions and the actual part.
The paper’s strongest argument is that manufacturability should enter the optimization itself, instead of showing up later in the process. As an example: build orientation affects overhangs, support volume, staircase surface error, build height, heat flow, and anisotropy at the same time. Yet many workflows choose orientation first and optimize geometry afterward. The review says there has been very limited work on solving both of these together.
That sounds like a lot of computation is required, and there will be. But a workflow producing a very lightweight part that is expensive to build and even more expensive to finish is not a good result.
The researchers cite one aviation rocker-arm lattice example, reported in a prior review, where an optimized variable-density lattice reduced weight by 23 percent, stress by 68 percent, and strain by 14 percent against the original lattice configuration.
And weight is only one factor. A lighter design can consume more support material, take longer to print, demand more machining, or introduce fatigue-sensitive surfaces. If it fails qualification or cannot be reproduced consistently, that fancy geometry has not really delivered the benefits.
I also noticed the researchers’ call for calibrated process maps instead of universal design rules. A fixed overhang angle is convenient for software, but whether a feature prints depends on the machine, material, layer thickness, energy input, and geometry. The same applies to minimum feature size and anisotropy. Optimization tools need constraints drawn from the actual production process, not generic rules inherited from somebody else’s machine. These are not features you’d find in typical slicing software.
AI may help here by sorting through parameters and machine characteristics. But an AI model trained on a small collection of builds would not be sufficient.
That amazing and complex generated design on the screen is still only the beginning. The best workflow will be the one that can print the part again, measure it, qualify it, and show that its total cost to produce and performance are both optimal.
Via Open Access Research Journal of Science and Technology