Material extrusion often has a problem: the 3D printer can appear to be working perfectly while actually building a failed part.
The nozzle moves, filament feeds, and layers accumulate. But an under-extruded section, poor layer bond, partial blockage, temperature drift, or wandering extrusion may not become obvious until the build is complete. By then, the material, machine time, and perhaps an entire production schedule have already been lost.
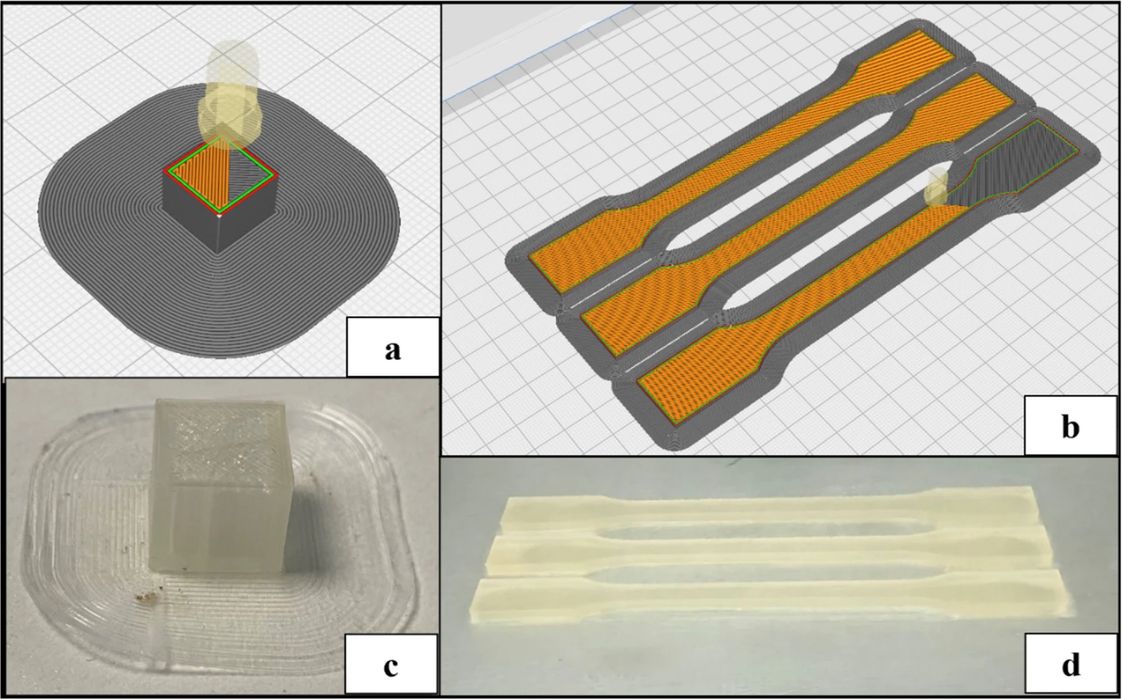
The research paper In-line monitoring of the material extrusion additive manufacturing process by non-destructive methodologies examines the gap between what the machine is doing and what the operator can actually know during a print.
The interesting part is the phrase “in-line”, which means observing the process in real time as the material is deposited, without the need to cut up the part to find a defect after the fact.
That is a difficult task, however.
A polymer extrusion is small, hot, moving and continually changing shape as it contacts the preceding layer. A monitoring system has to identify a real problem from normal variations caused by toolpath direction, corners, acceleration, cooling, illumination, or the geometry underneath the current layer.
The researchers consider non-destructive approaches for observing the material extrusion process. These methods can include optical observation of extrusions, thermal sensing of the newly extruded material, and other sensor-based signals that reveal whether the process is behaving as expected. Each is effectively looking at a different part of the same event.
A camera can potentially see whether the extrusion is where it should be and whether its width appears consistent. Thermal observation can reveal a different issue: whether the material is arriving and cooling within the expected temperature window. That could be particularly useful for layer bonding, because polymer layers do not fuse equally well if the previously deposited surface has cooled too far.
Neither type of observation alone is a magic defect detector. An extrusion may look acceptable from above while having a weak bond below it. A hot region may be entirely normal at a tight corner where the nozzle slows down. Somehow you have to convert a sensor signal into a reliable process judgement.
That is why in-line monitoring is really a software and decision problem as much as a sensor problem. The system needs a reference for normal behavior, an ability to recognize departures from that behavior, and some tolerance for harmless variations that naturally occur. You don’t want alarms when there is nothing truly bad happening.
The most useful outcome would not necessarily be fully automatic correction during the print job. Even a system that flags a suspect region, records its location, and lets an operator decide whether to pause or continue would be a huge improvement over discovering an issue after the build.
There is a another possibility. If the printer can link a detected anomaly to GCODE position and process conditions, it could begin to build a traceable record of each part. For production work, that may be more valuable than a simple pass-or-fail image. You would know where an event occurred, what the nozzle temperature and motion conditions were, and whether a corrective action followed. From this you could potentially tweak print parameters to avoid the same situation in future builds.
FFF has spent decades assuming that a commanded extrusion is actually what happens, but as we all know, that is rarely the case. This research shows methods of monitoring FFF system performance that just might make its way into future systems.
Via The International Journal of Advanced Manufacturing Technology